Explore our engineered chemical agents manufactured under strict ISO quality controls, designed specifically for heavy industrial applications, metal extraction, leaching, and blasting applications.
The modern mining and mineral processing industry is undergoing a structural paradigm shift. As global demand for critical transition metals—such as copper, lithium, nickel, cobalt, and rare earth elements (REEs)—continues to surge, extractive metallurgists and mine operators face deteriorating ore grades and increasingly complex mineral matrices. Consequently, the reliance on high-precision chemical reagents, hydrometallurgical leaching agents, oxidation regulators, and explosive precursors has reached an unprecedented high.
Transition from traditional pyrometallurgical smelting to low-carbon hydrometallurgical leaching requires ultra-pure reagents like nitric acid, sodium nitrate, and metal nitrate oxidizers to maximize recovery rates from complex sulfide and oxide ores.
Global mining conglomerates (BHP, Rio Tinto, Vale) strictly audit reagent suppliers for ESG compliance, requiring zero-impurity raw materials that reduce tailings toxicity and minimize process emissions.
One-size-fits-all chemicals fail in localized geology. Custom OEM chemical exporters provide site-specific tailored concentration ratios, proprietary additives, and controlled dissolution rates.
Henan Yongchang Nitro Fertilizer has established a world-class chemical synthesis matrix driven by automation, digital monitoring, and chemical engineering innovation. Operating continuous synthesis pipelines for concentrated nitric acid (300,000 tons/yr) and dilute nitric acid (500,000 tons/yr), our facilities guarantee price stability, continuous mass production, and strict assay tolerances for international buyers.
By integrating proprietary Dual-Pressure Nitric Acid Processes, our manufacturing footprint achieves unprecedented thermal efficiency while drastically reducing NOx emissions and carbon intensity—providing OEM clients with low-carbon chemicals essential for scope 3 emission auditing.
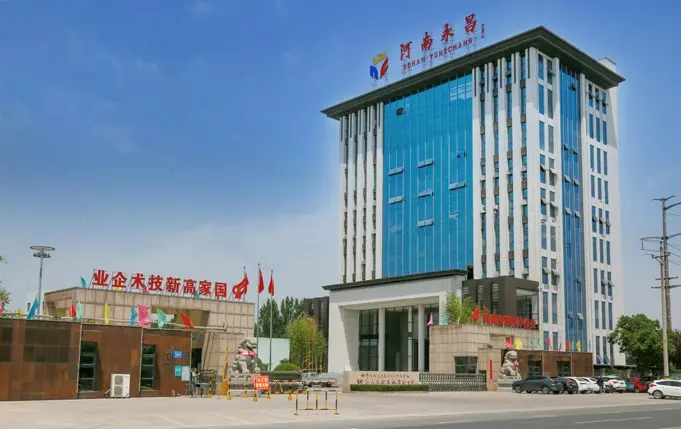
Henan Yongchang's 2025 Smart Digital Production Complex

Proprietary Dual-Pressure Nitric Acid Process significantly reduces primary energy consumption while guaranteeing chemical assay stability across industrial shipments.

Pioneered nitrogen-phosphorus and specialized inorganic salt crystallization tech, optimizing purity for industrial smelting and technical applications.

100+ customized industrial formulas with end-to-end quality control, from raw material synthesis to bulk vessel loading and destination port logistics.
Our OEM mining chemical portfolio is specifically optimized for severe operational environments, variable ore chemistry, and distinct extraction technologies globally:
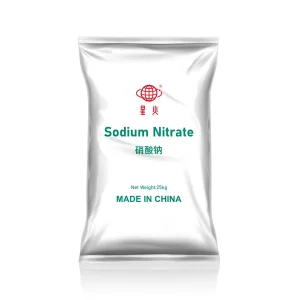
In heap leaching and agitation leaching of refractory copper-cobalt oxide and sulfide ores, maintaining oxidation potential is vital. Our high-purity White Fuming Nitric Acid (HNO3) and Sodium Nitrate serve as powerful oxidizing agents to convert low-solubility cuprous/cobaltous species into highly soluble ionic forms, boosting leach kinetics by up to 22% while suppressing unwanted iron dissolution.
For refractory gold cyanidation circuits, oxygen depletion in slurries limits recovery. The application of technical-grade Calcium Nitrate Granular and chemical oxidizers helps passivate reactive sulfide minerals (pyrite/arsenopyrite), reducing cyanide consumption by up to 30% and eliminating toxic gas generation in leaching tanks.
The conversion of spodumene concentrate and brine into lithium hydroxide and battery-grade lithium carbonate requires zero-chlorine, low-heavy-metal salt solutions. Our Industrial-Grade Potassium Nitrate and Sodium Nitrate (Molten Salt Grade) provide unmatched chemical purity for high-temperature thermal extraction and purification steps.
Modern open-pit and underground mining operations rely heavily on stable ANFO and emulsion explosive formulations. Henan Yongchang supplies industrial-spec Ammonium Nitrate and Urea Ammonium Nitrate (UAN) solutions engineered for precise prill porosity, optimal fuel absorption, and maximum detonation velocity (VoD).
Founded in 1974, Henan Yongchang Nitro Fertilizer has evolved over half a century into a modern chemical manufacturing titan with an annual production capacity exceeding one million metric tons. Spanning foundational chemical synthesis to specialized mining reagents and modern nitro-compounds, we deliver total end-to-end supply chain reliability.
Implementing our "Localized Service + Global Footprint" strategy, our international sales network serves customers across 20+ countries and regions. We maintain full international compliance, ensuring seamless customs clearance and safety handling for hazardous and non-hazardous chemical shipments.
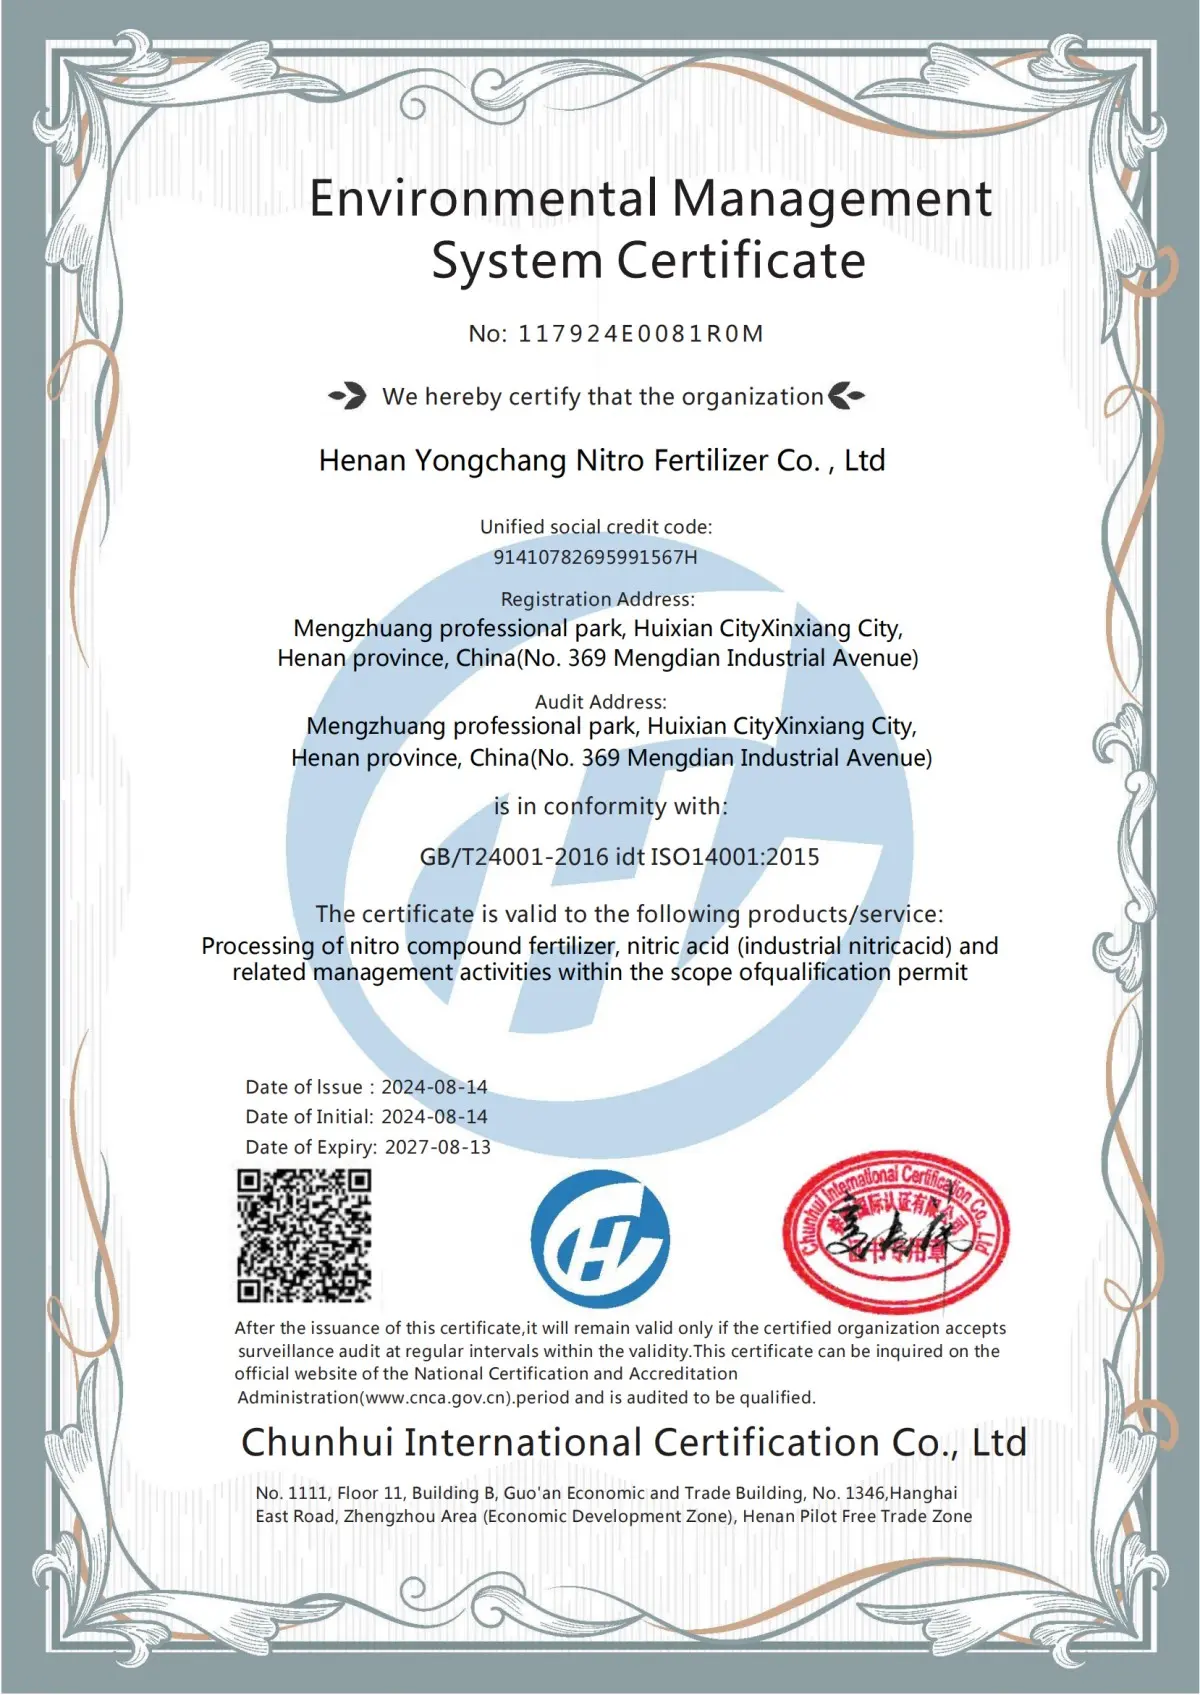
ISO Quality Management
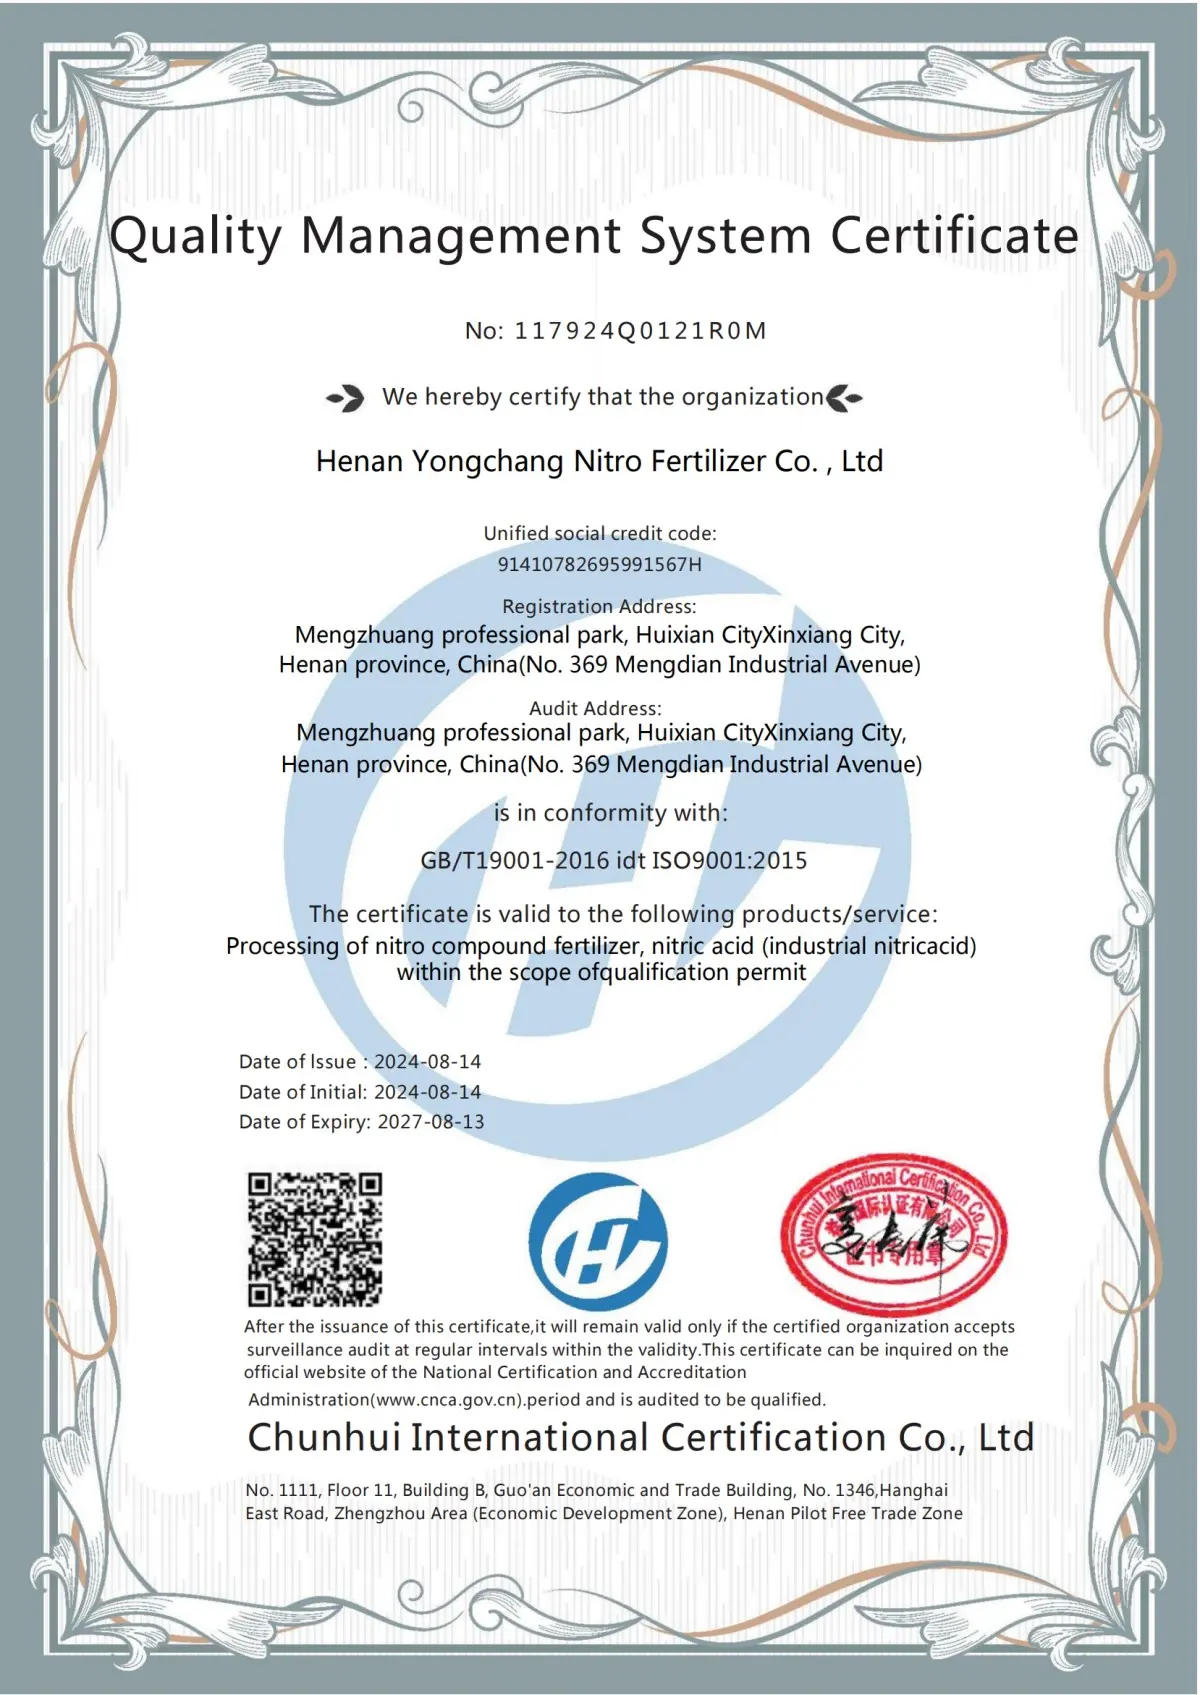
ISO Environmental Standard
Global Logistics & Distribution Hub Connectivity
Get authoritative engineering answers to common procurement, technical integration, and chemical handling queries from our technical team.
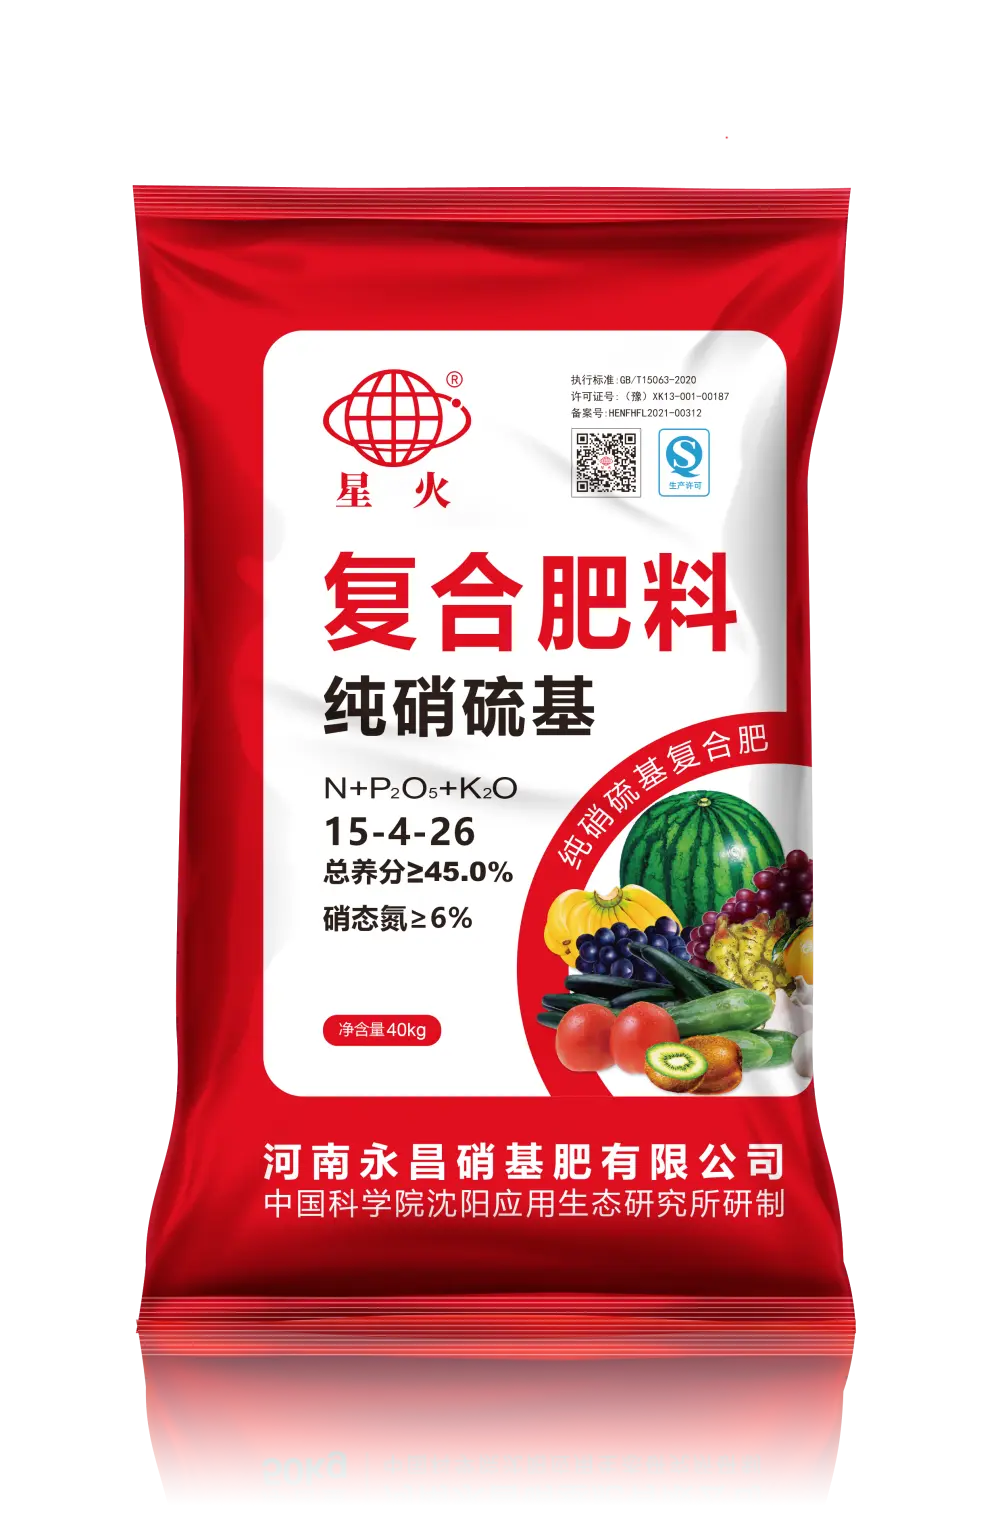
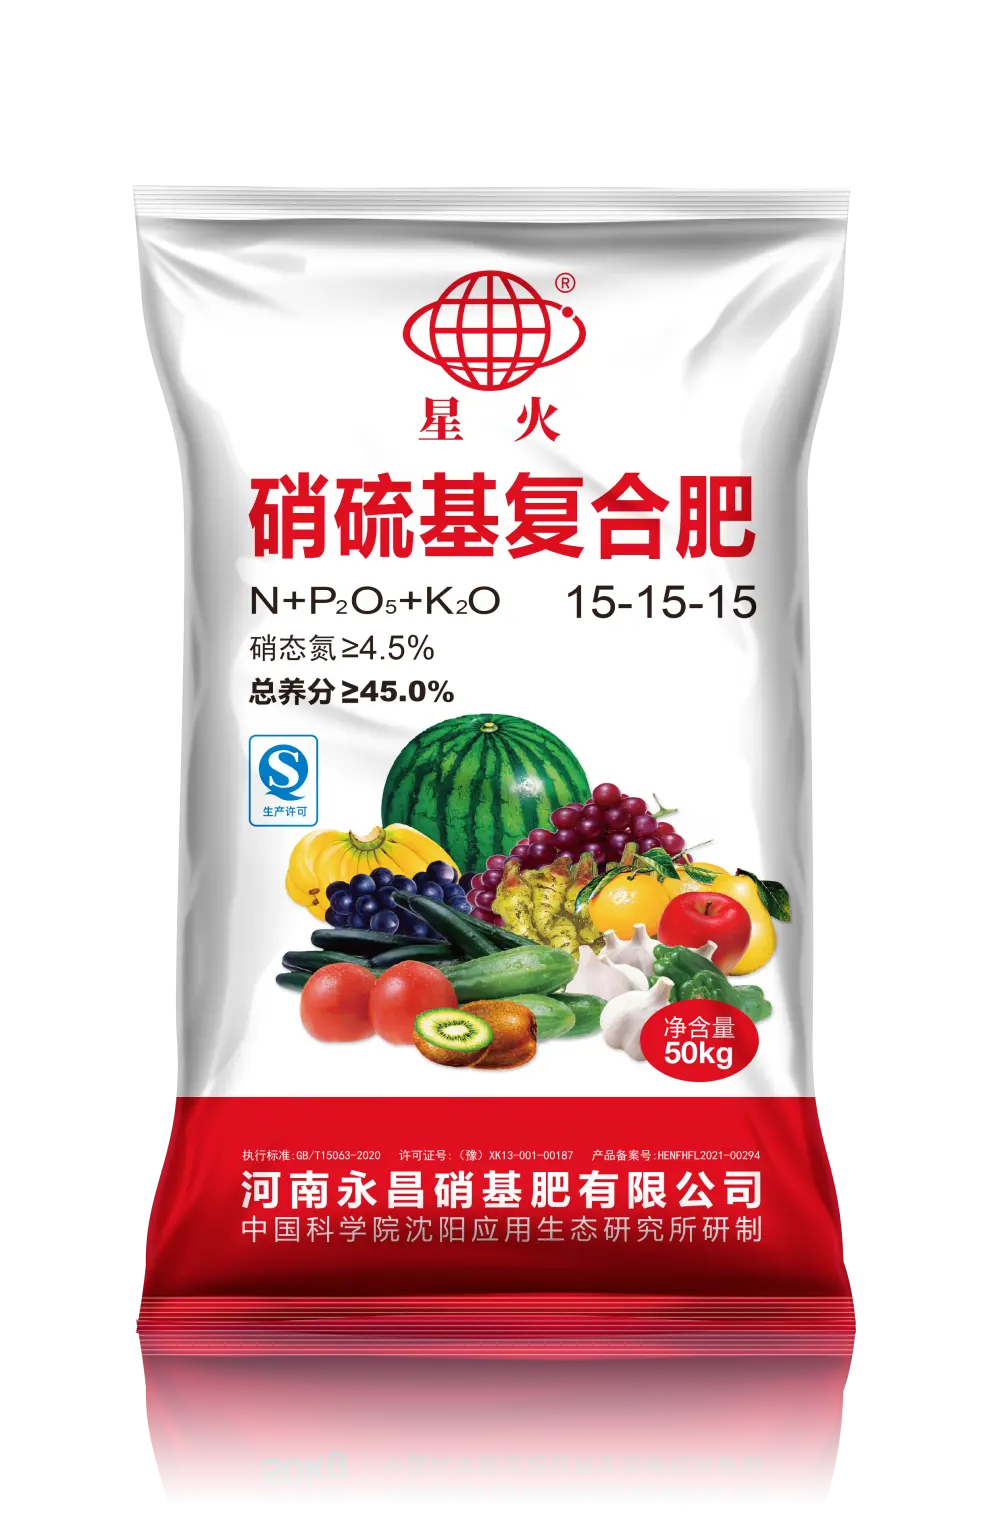
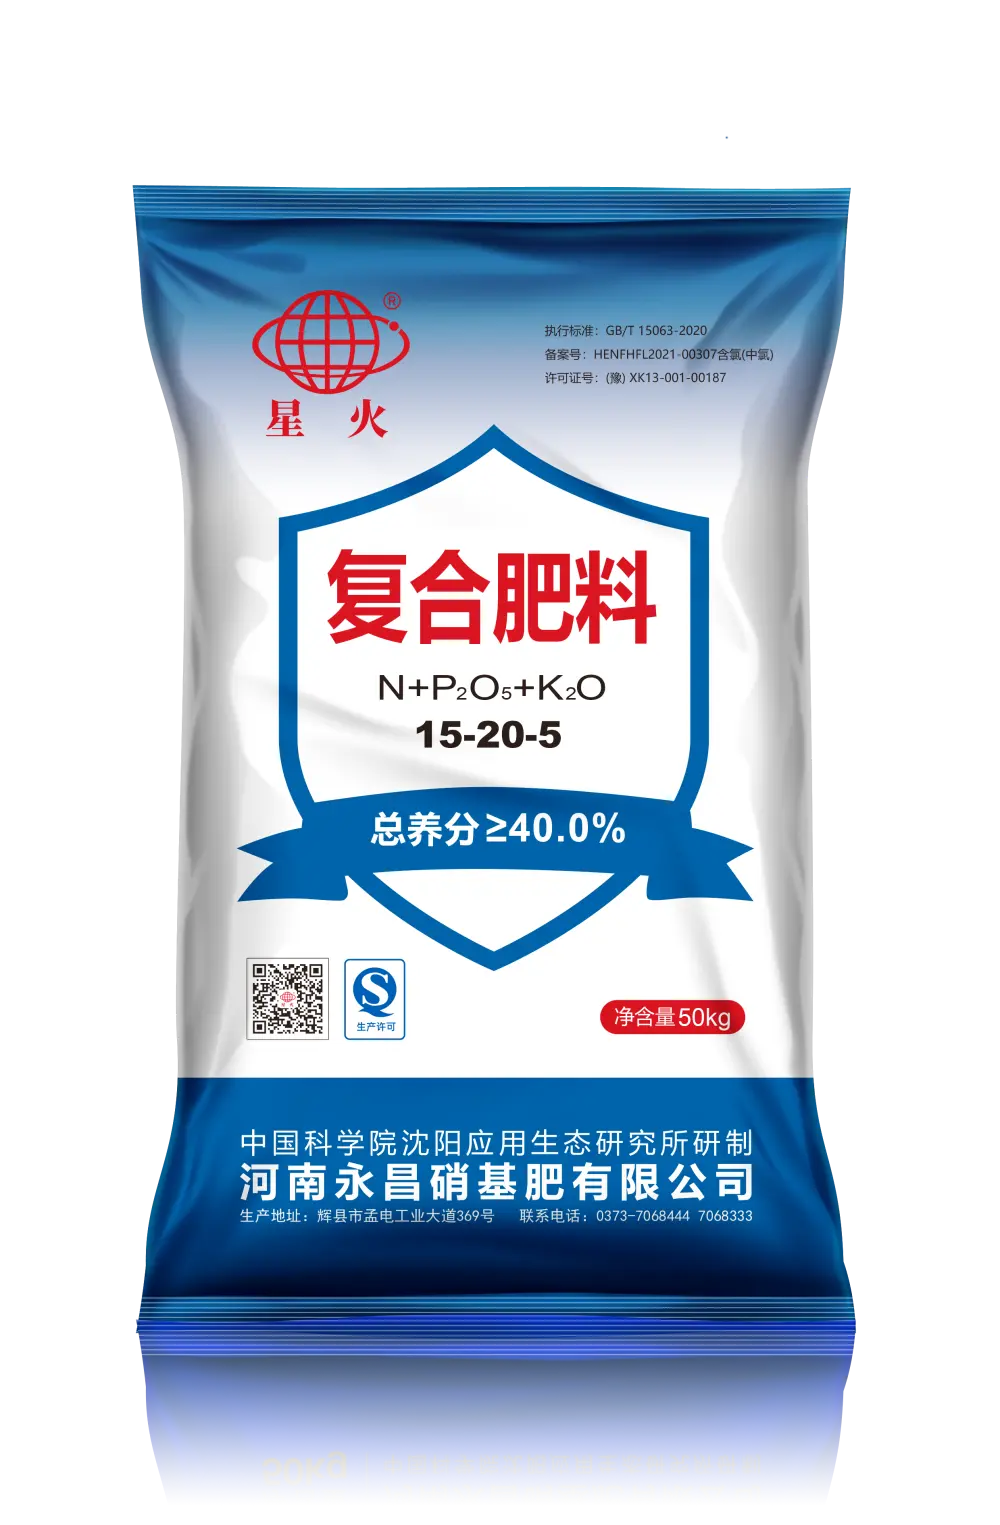
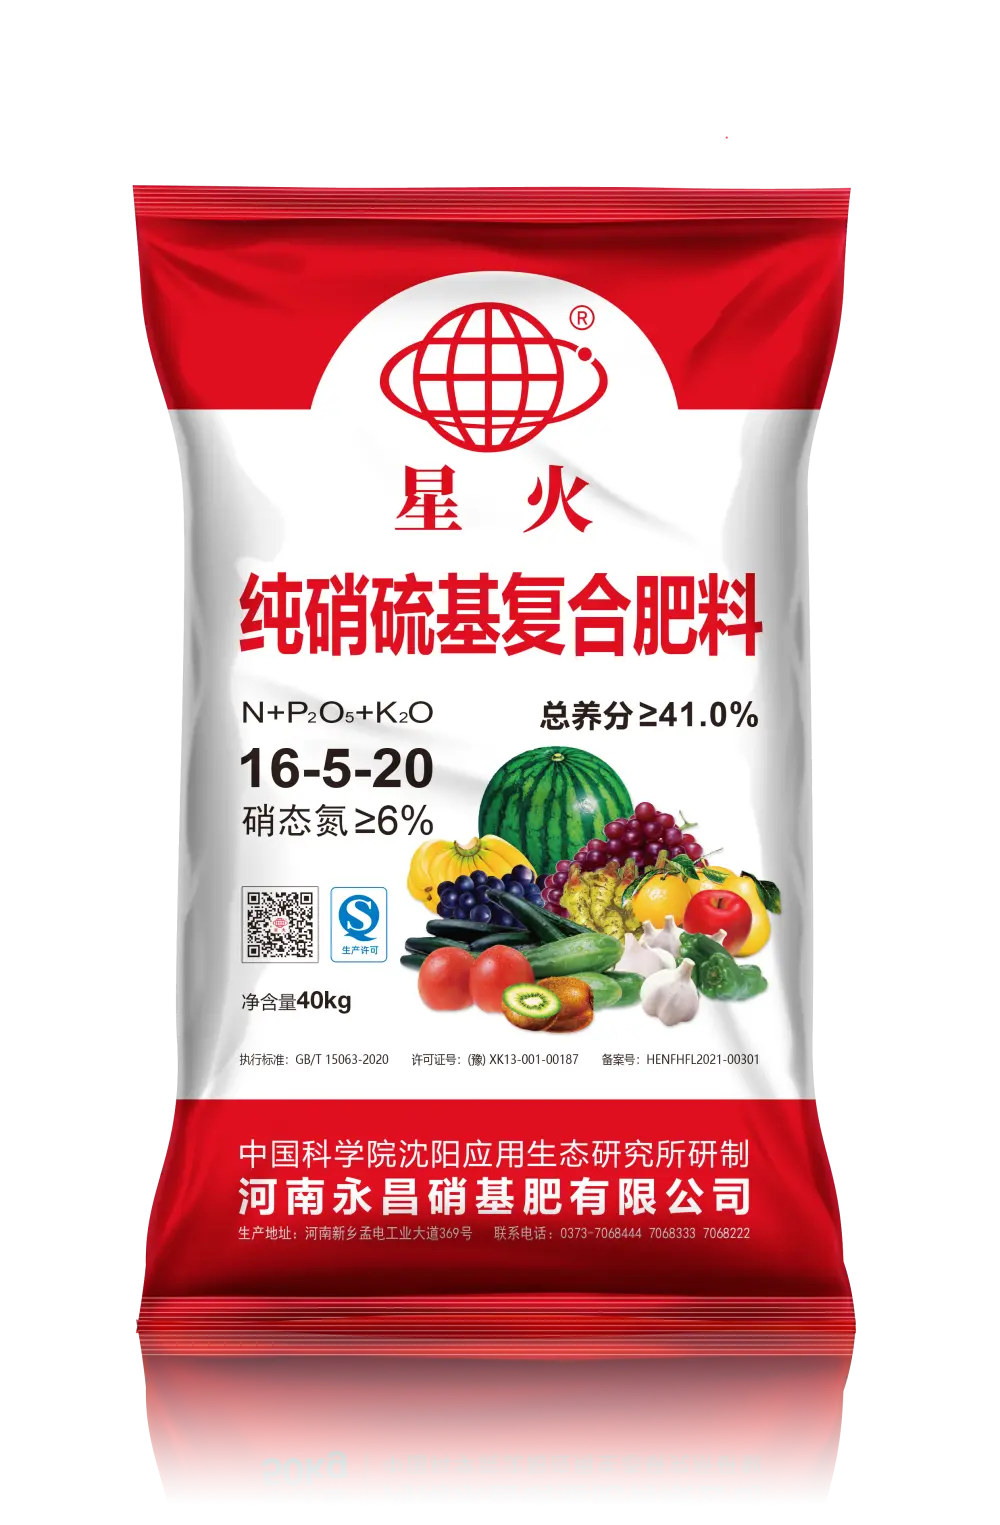
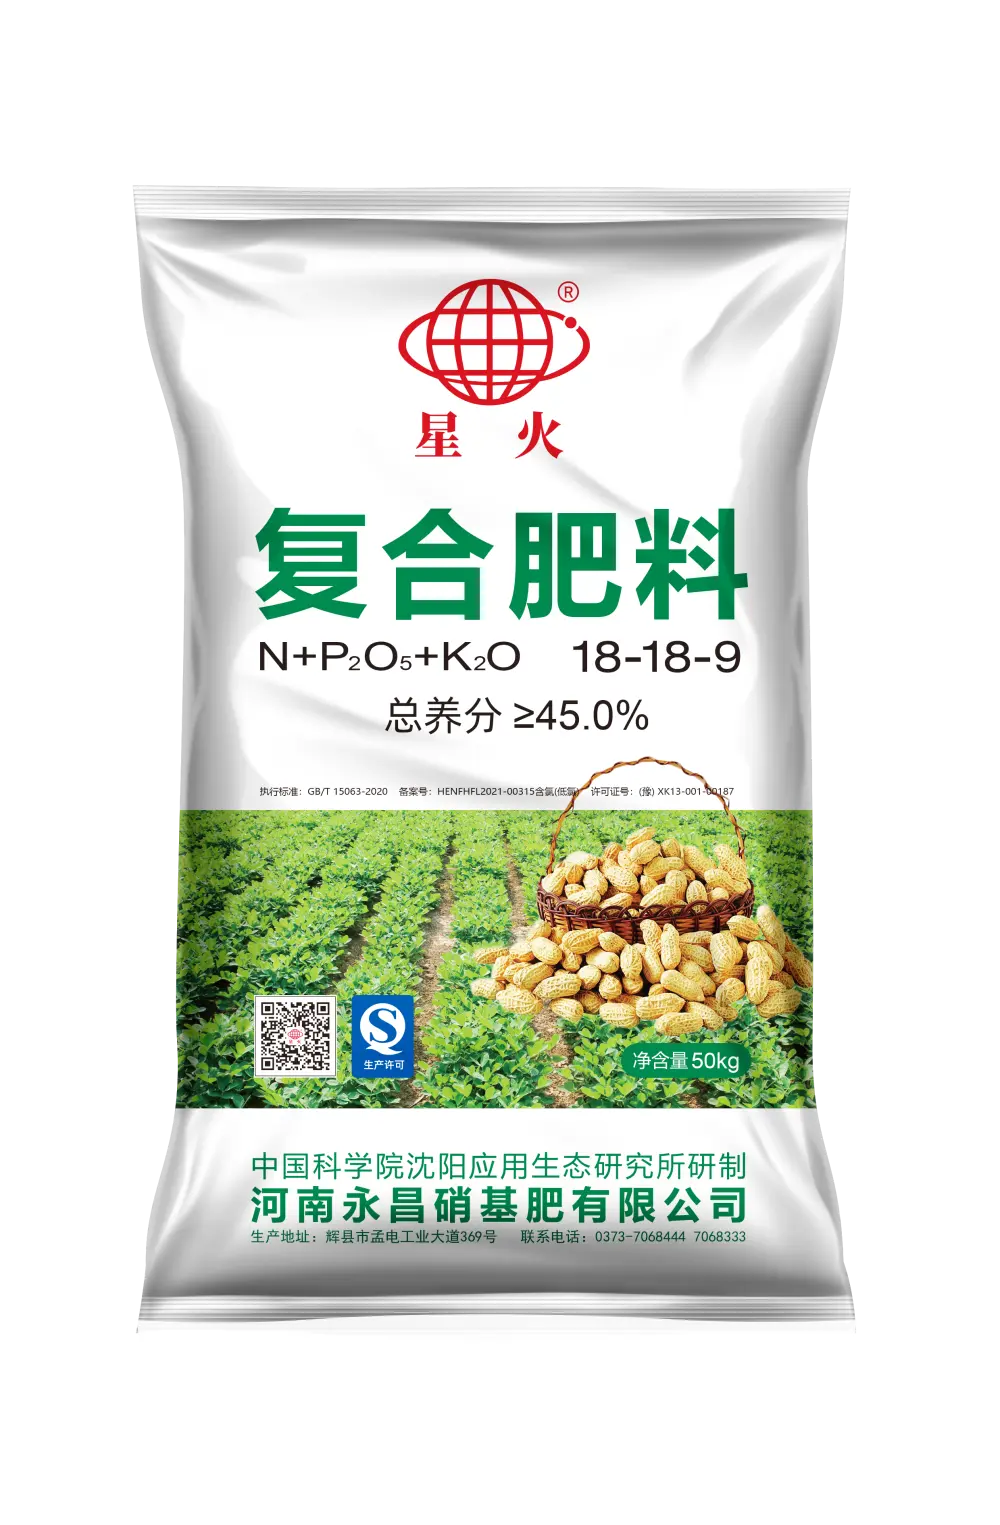
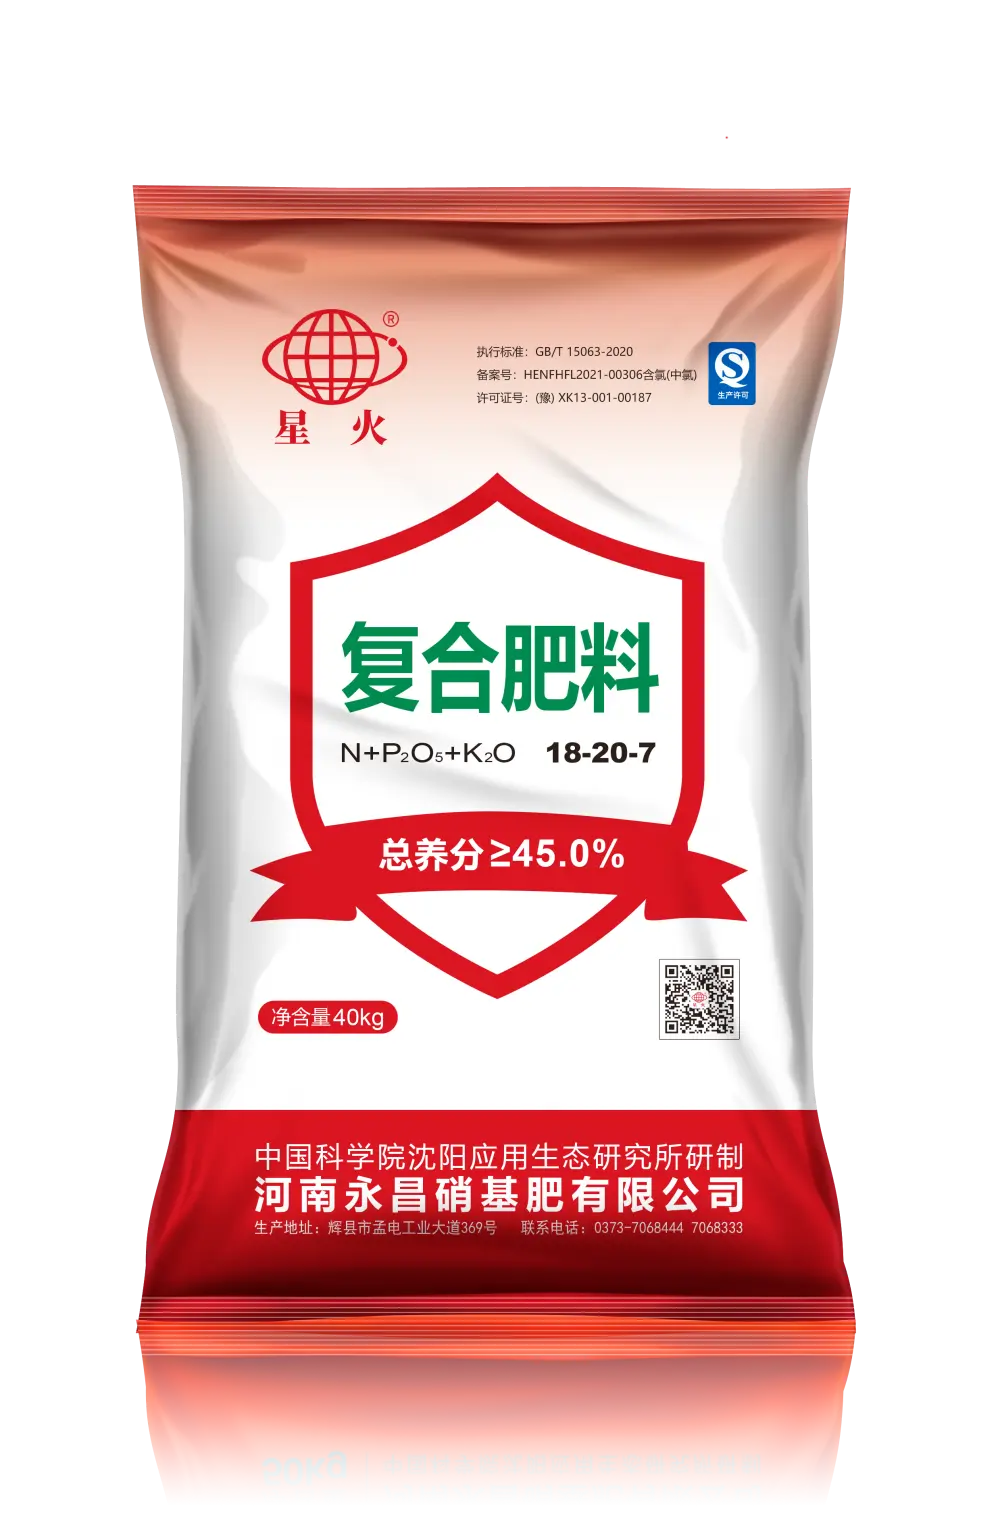
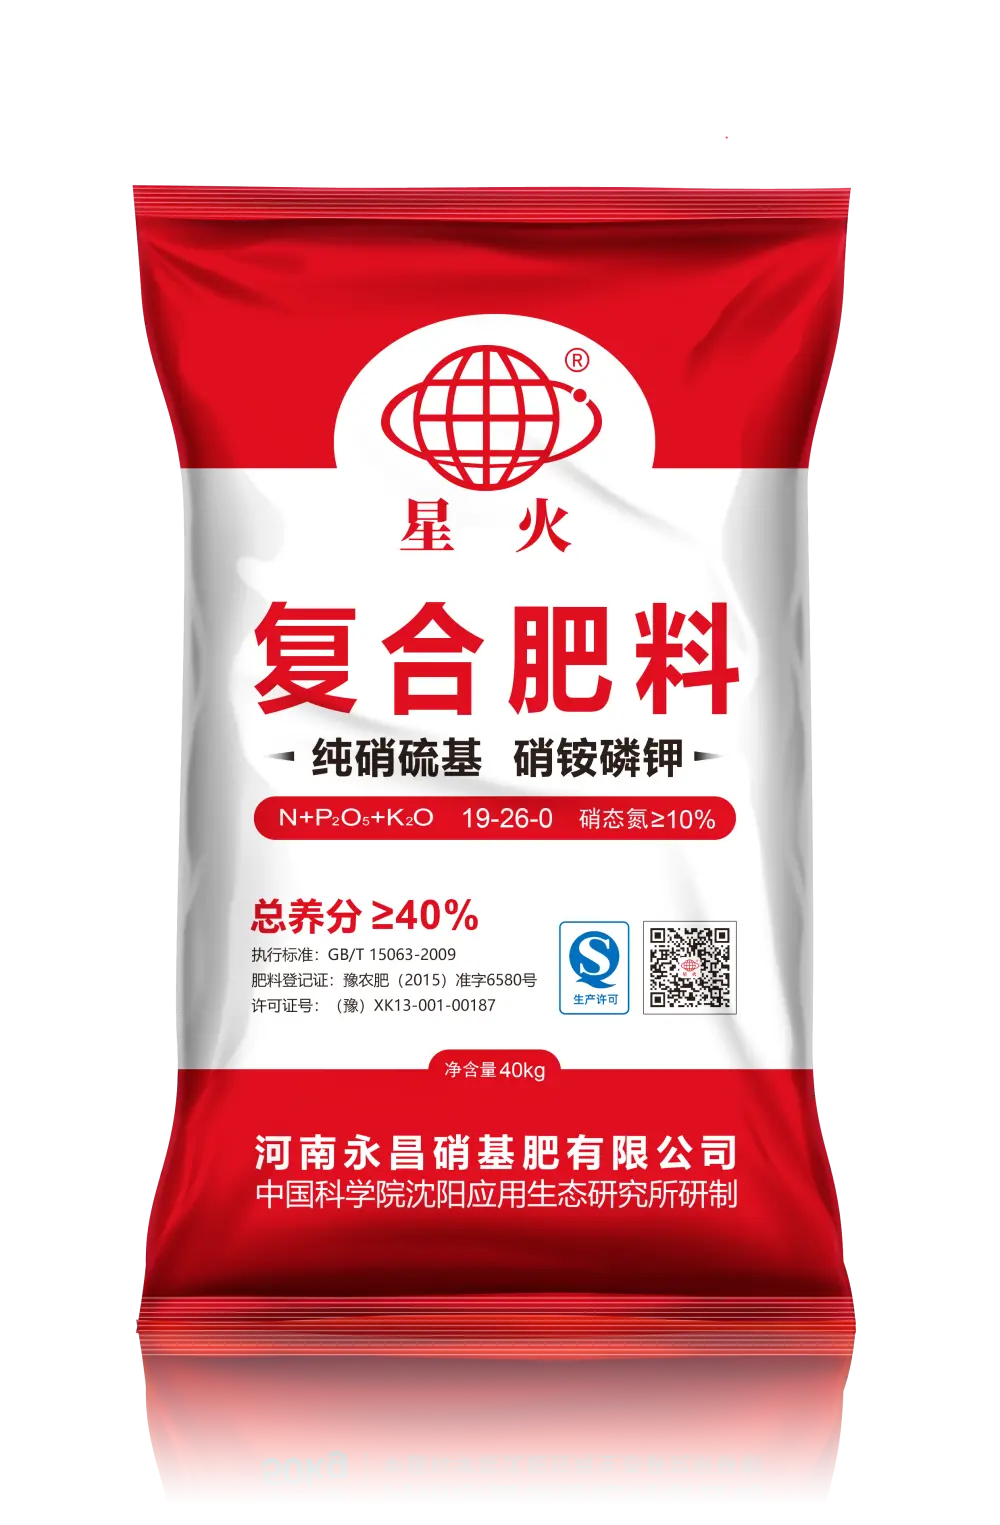
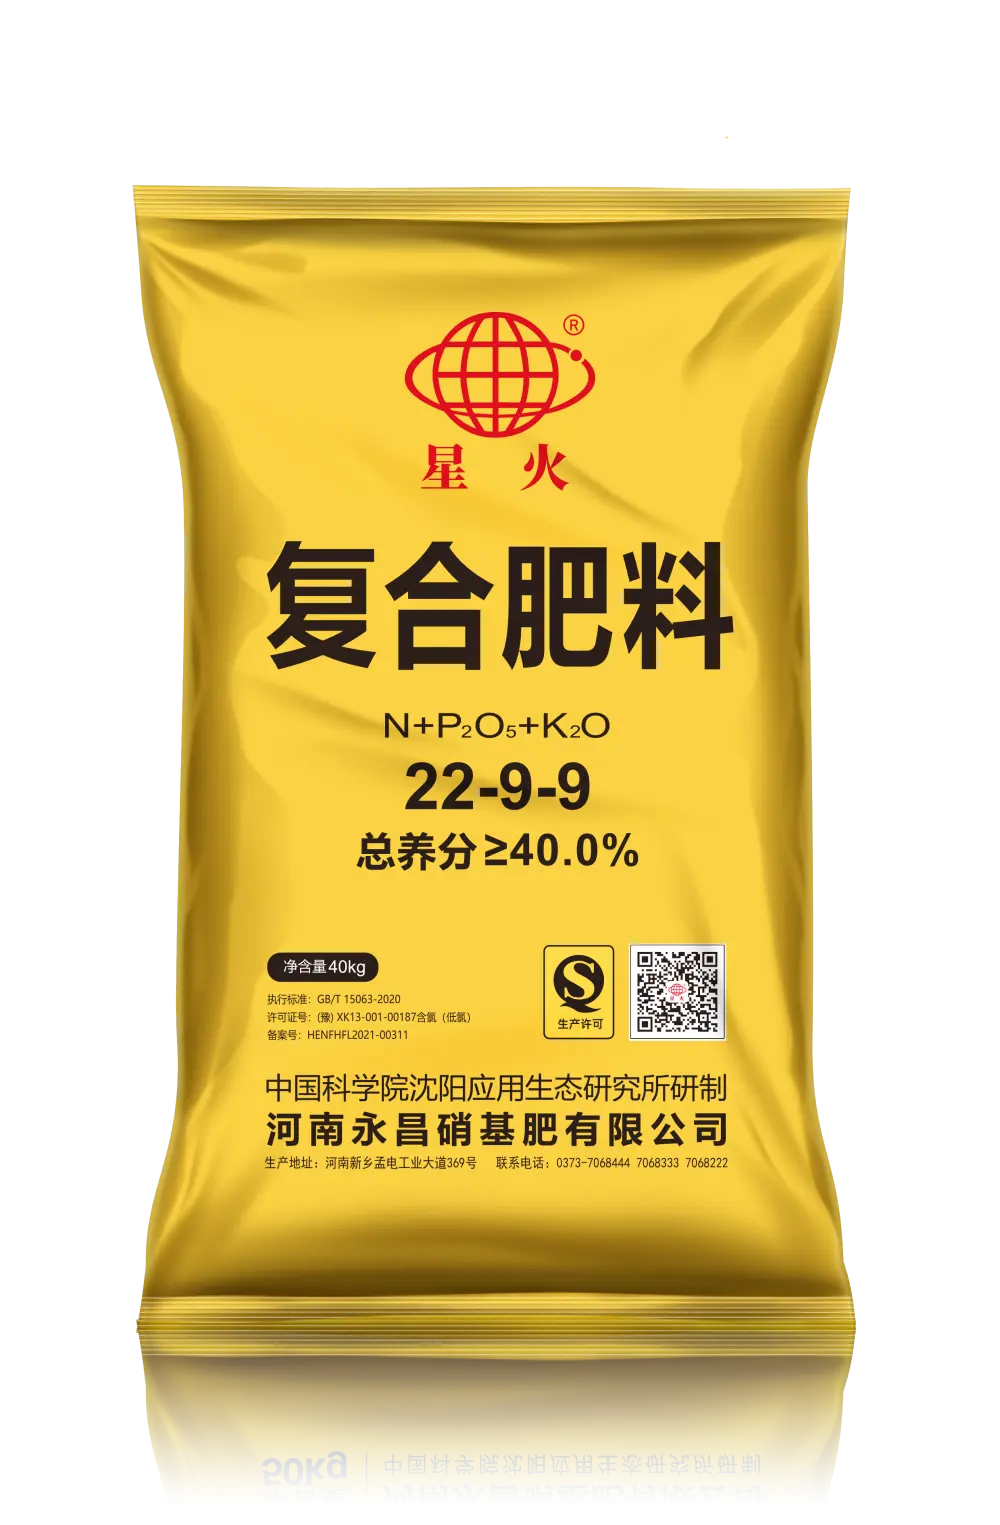
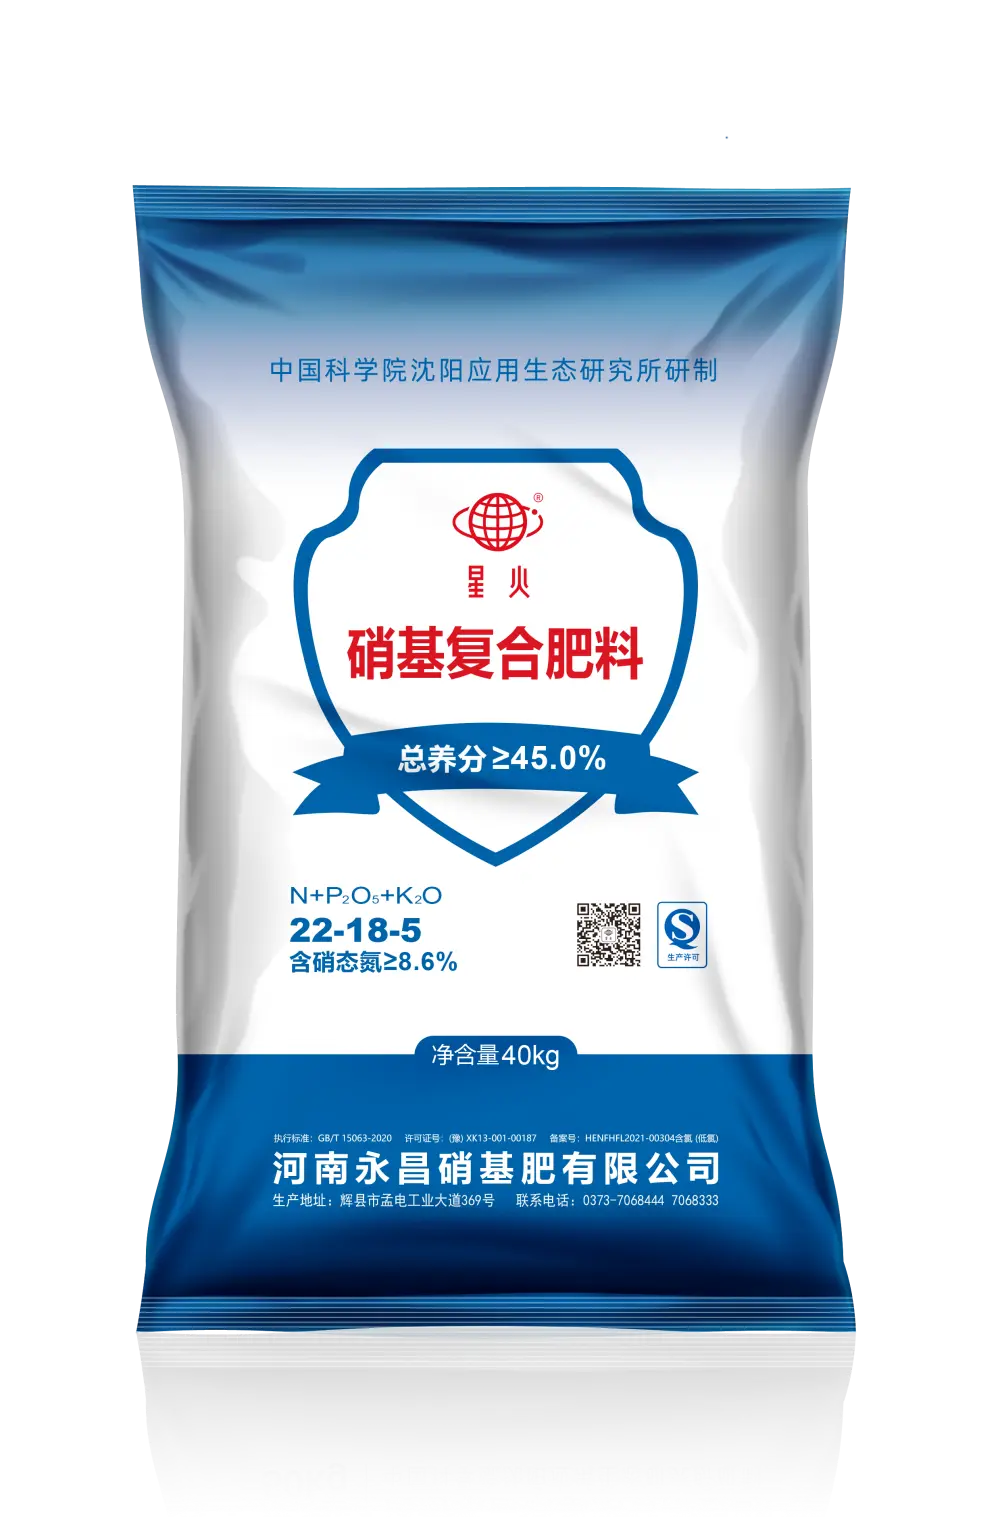
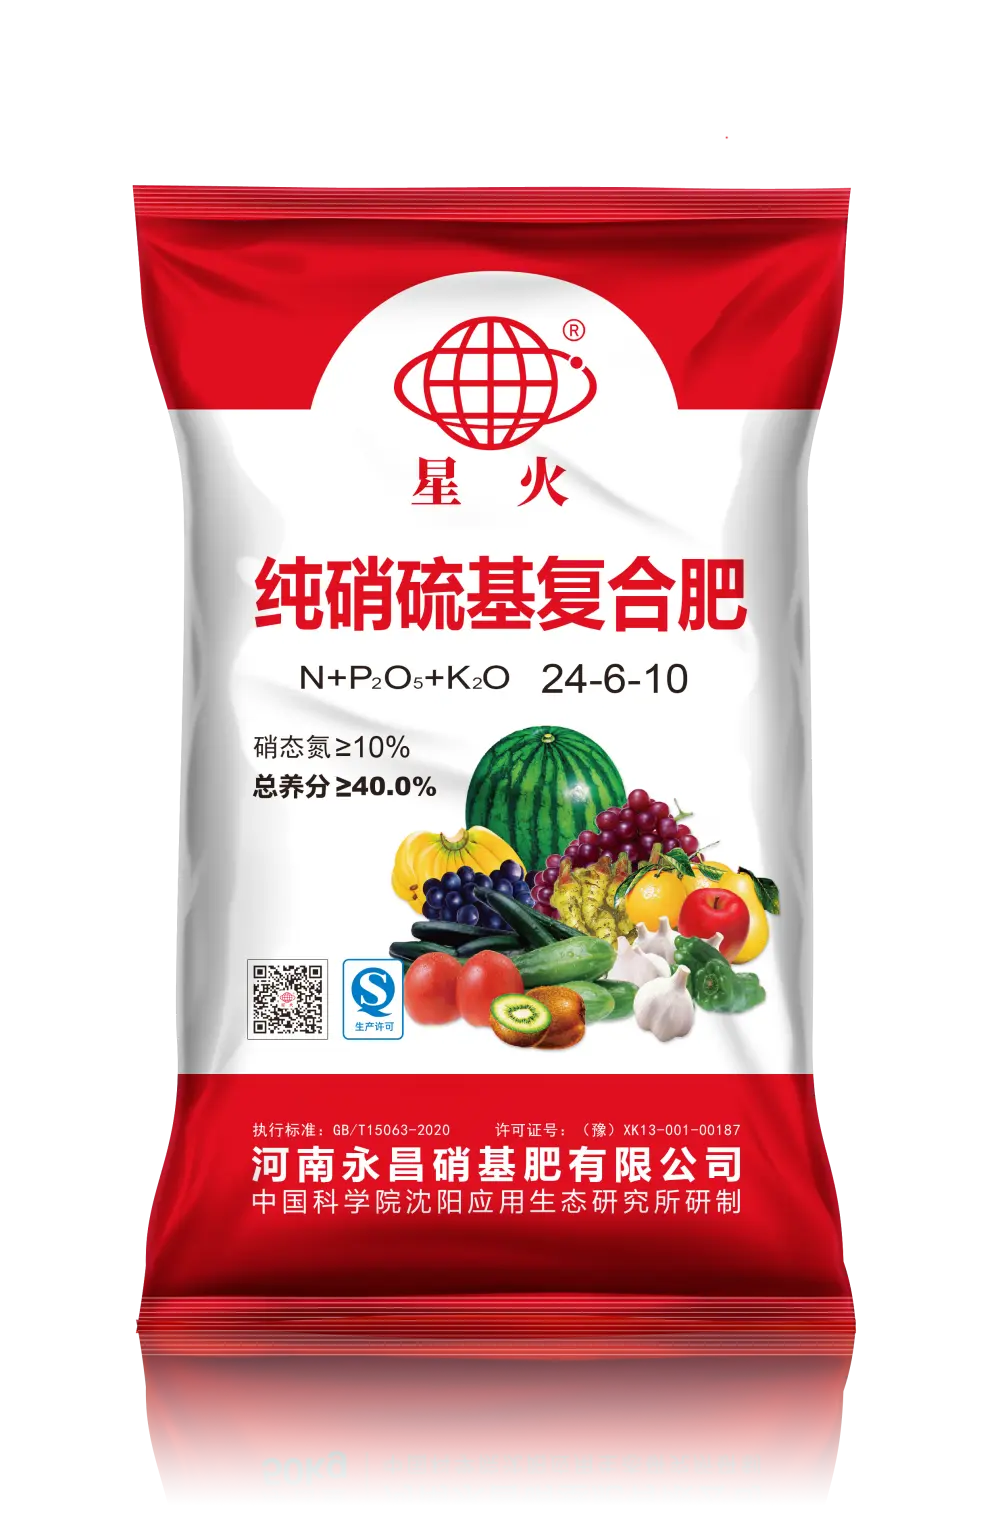
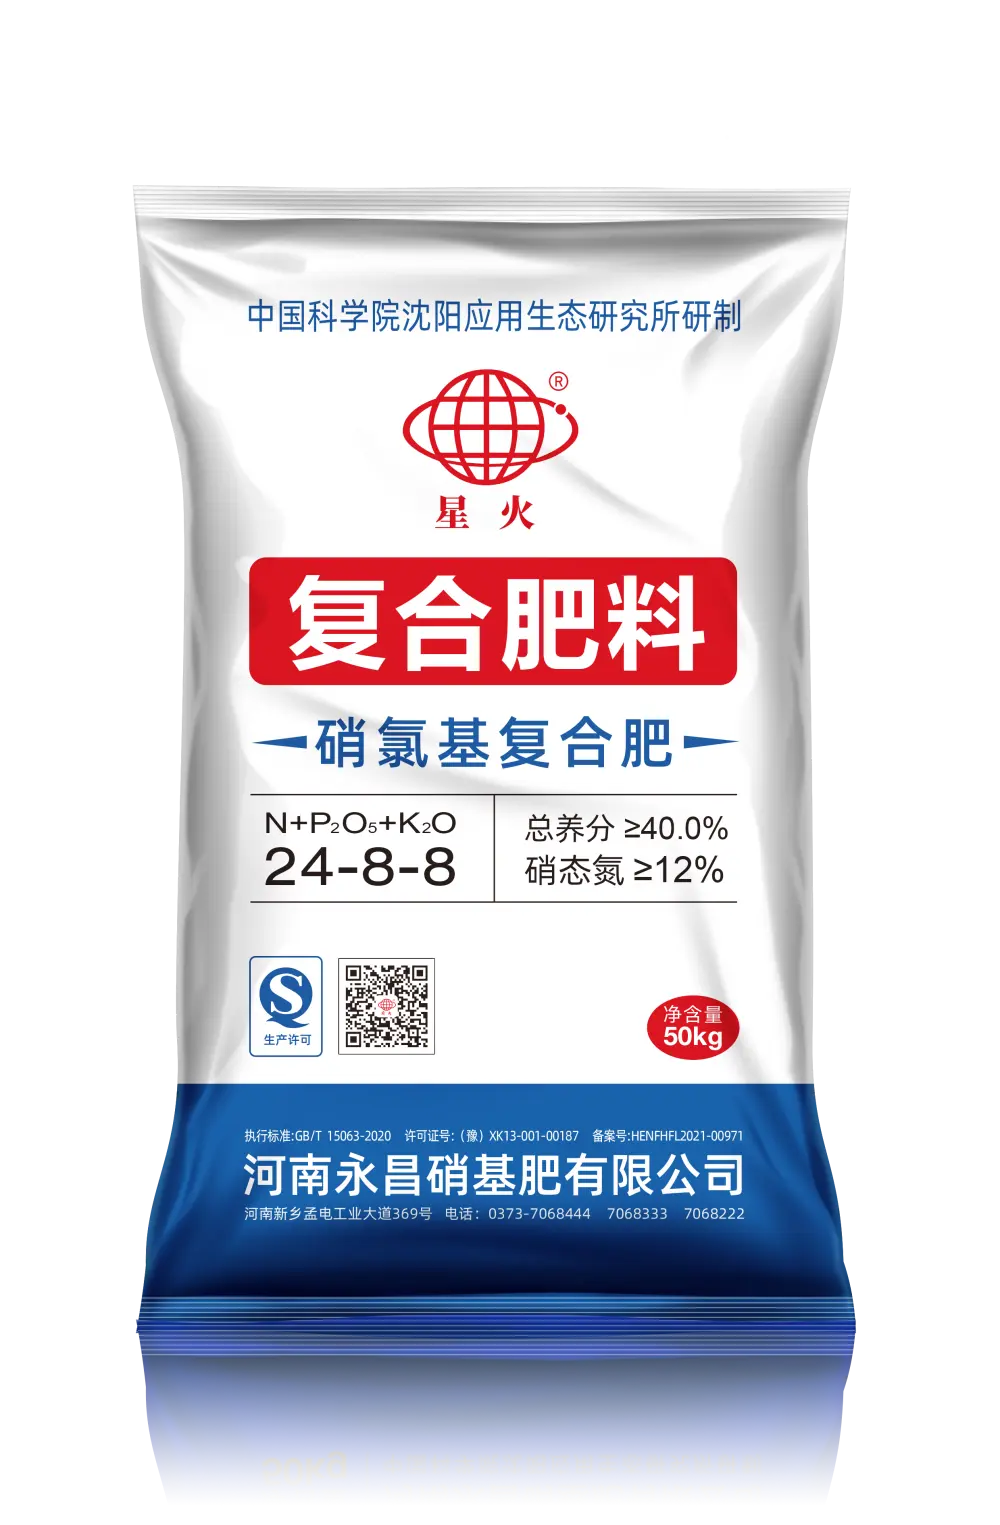
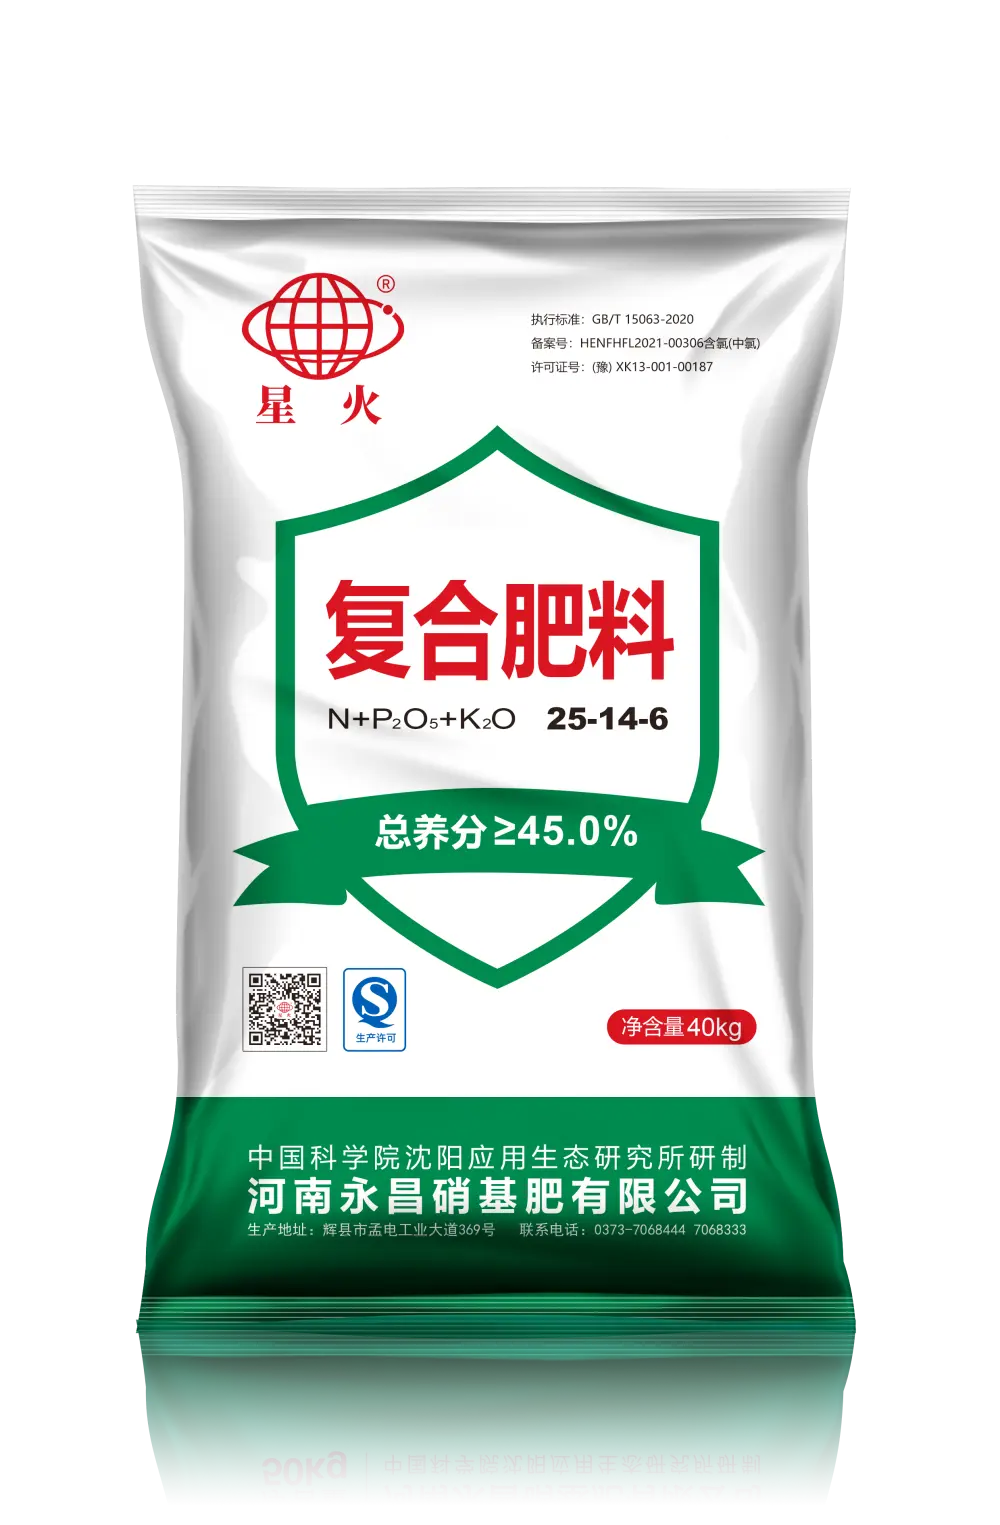
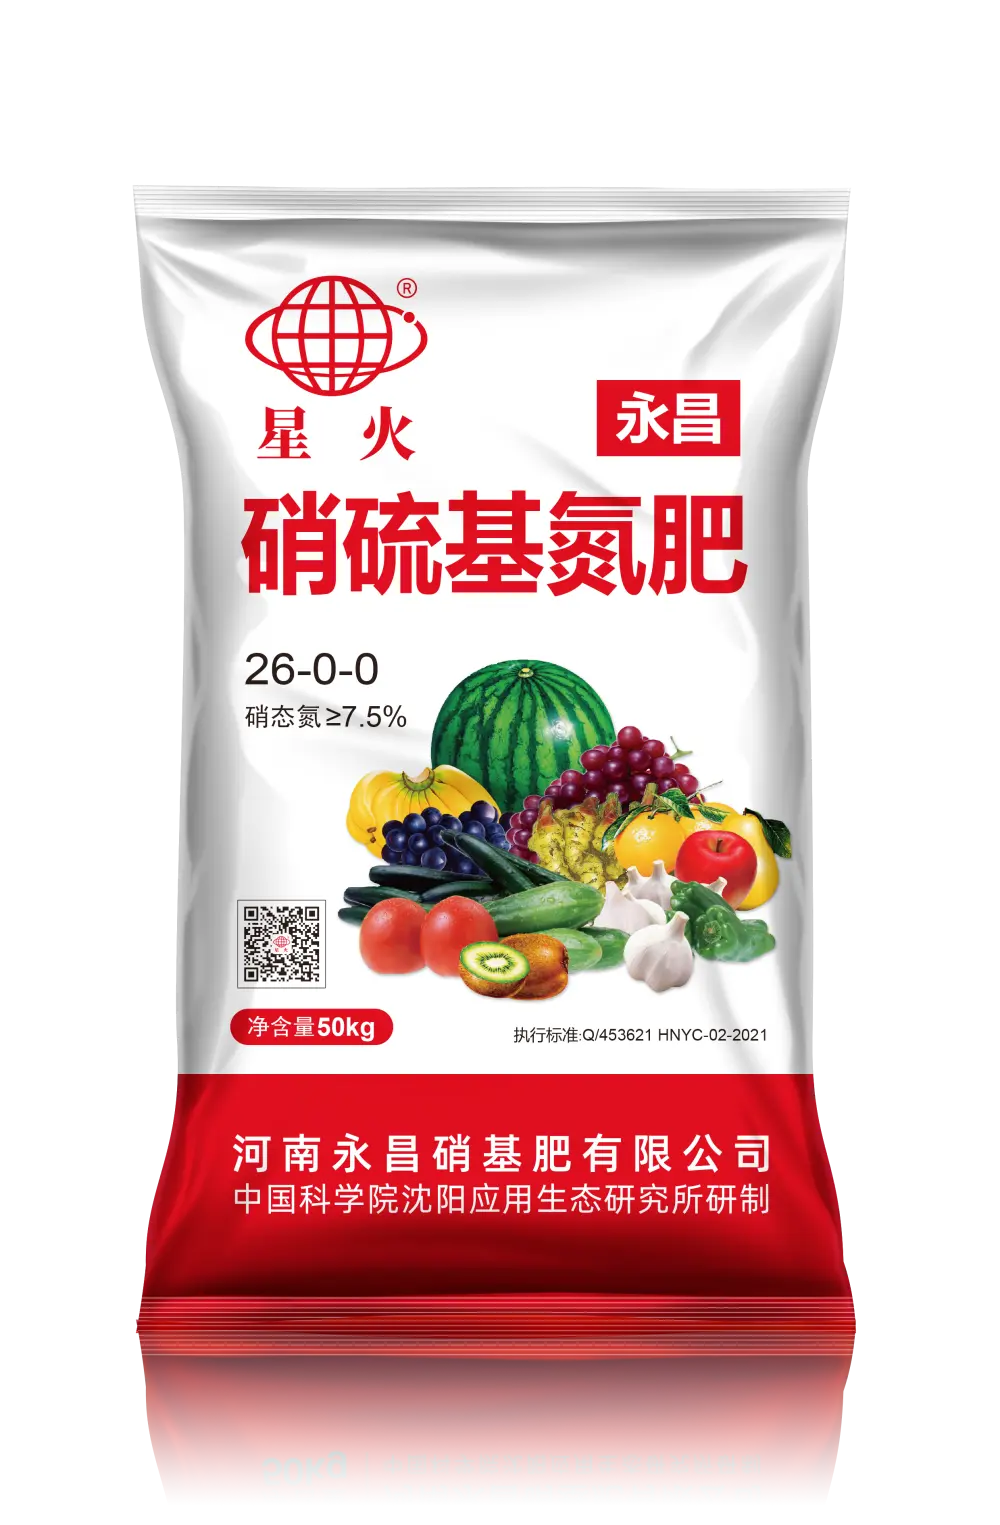
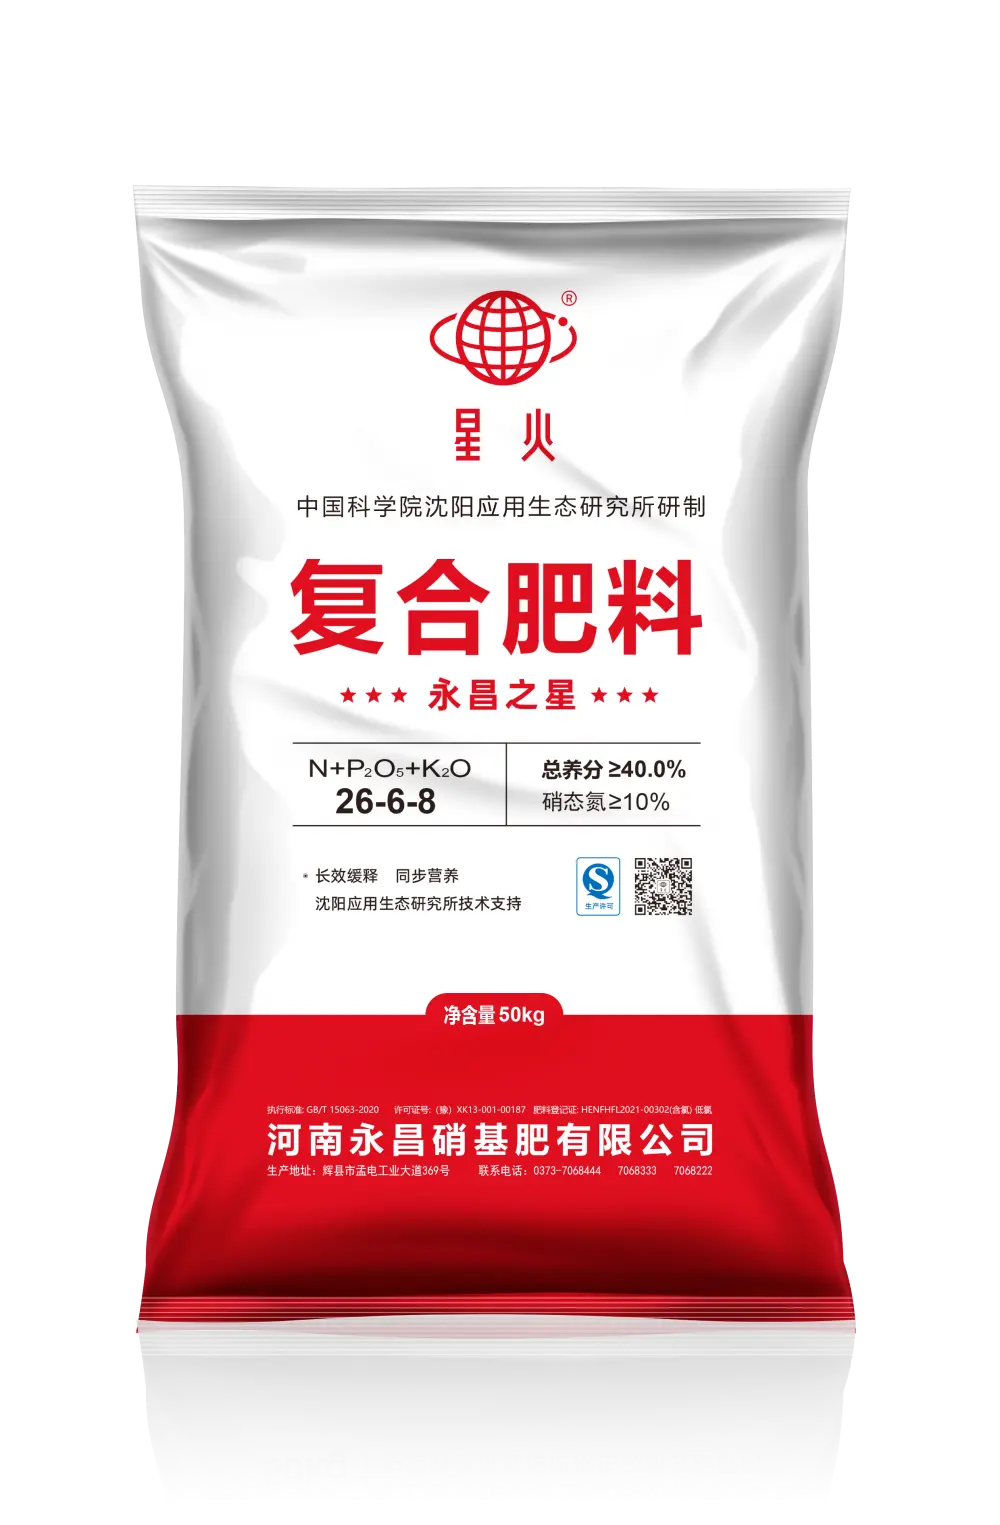
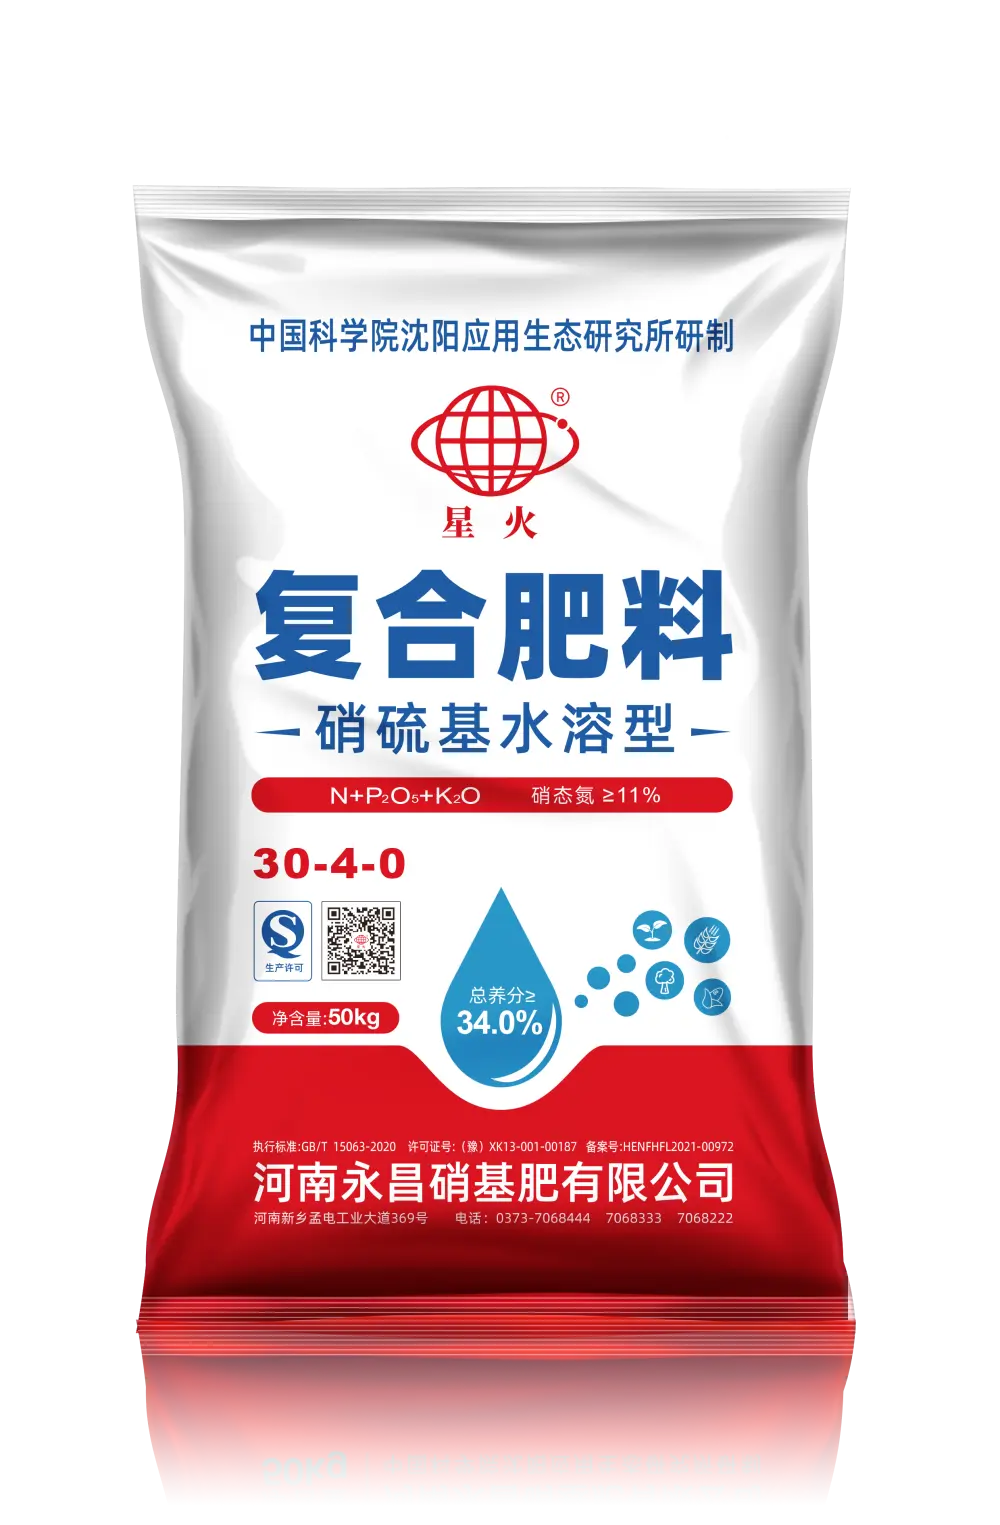
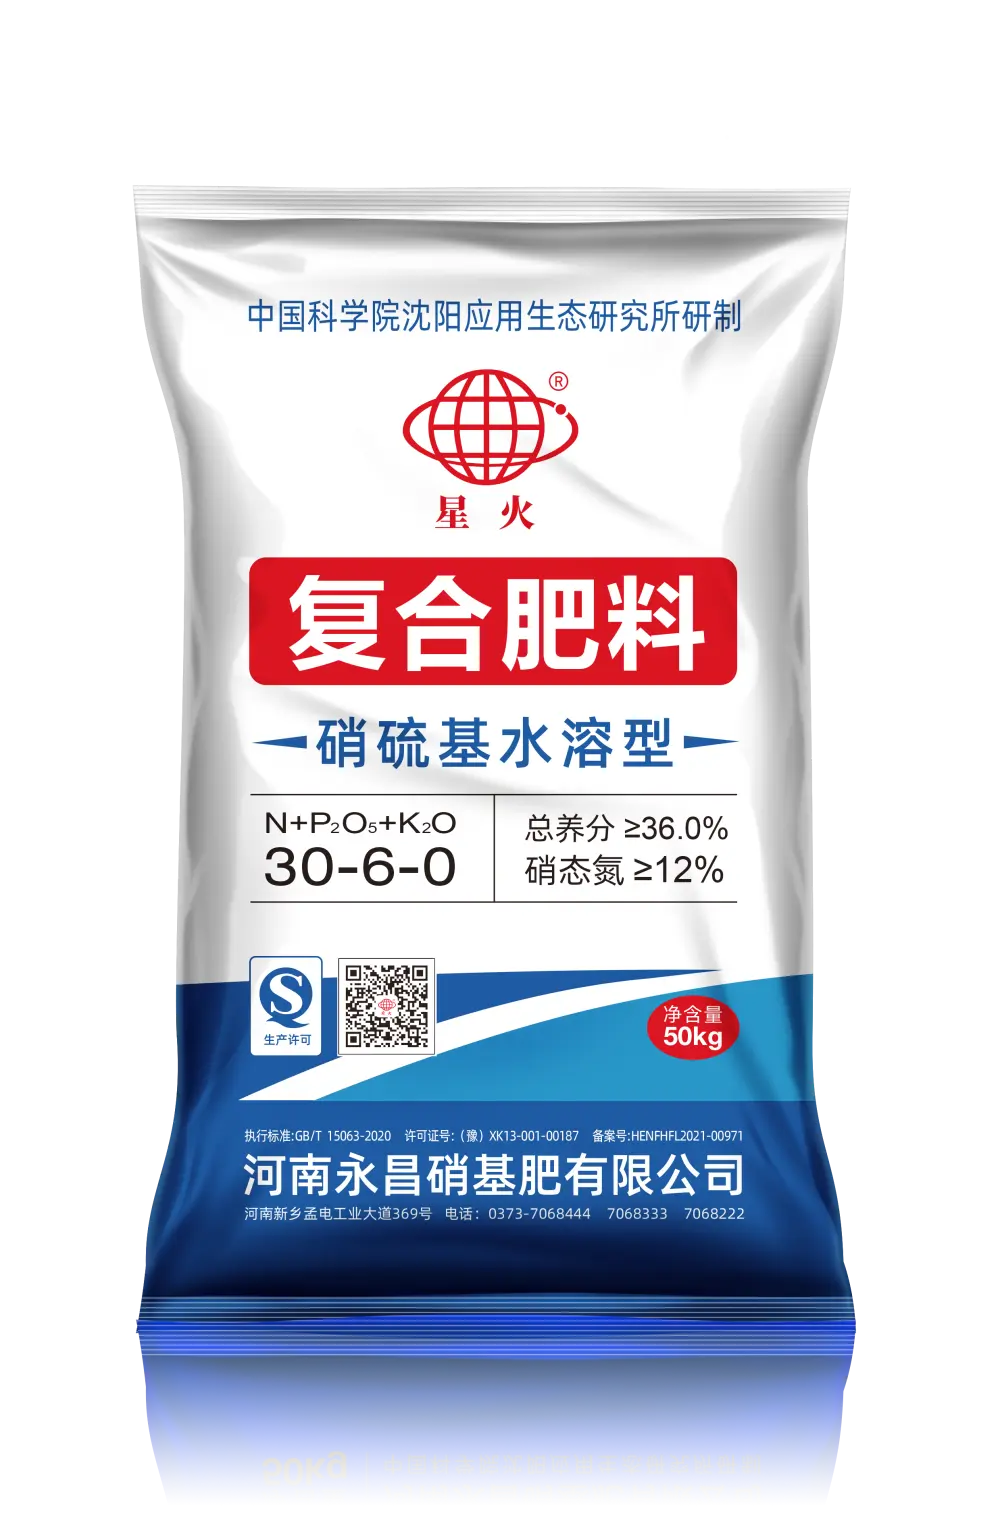
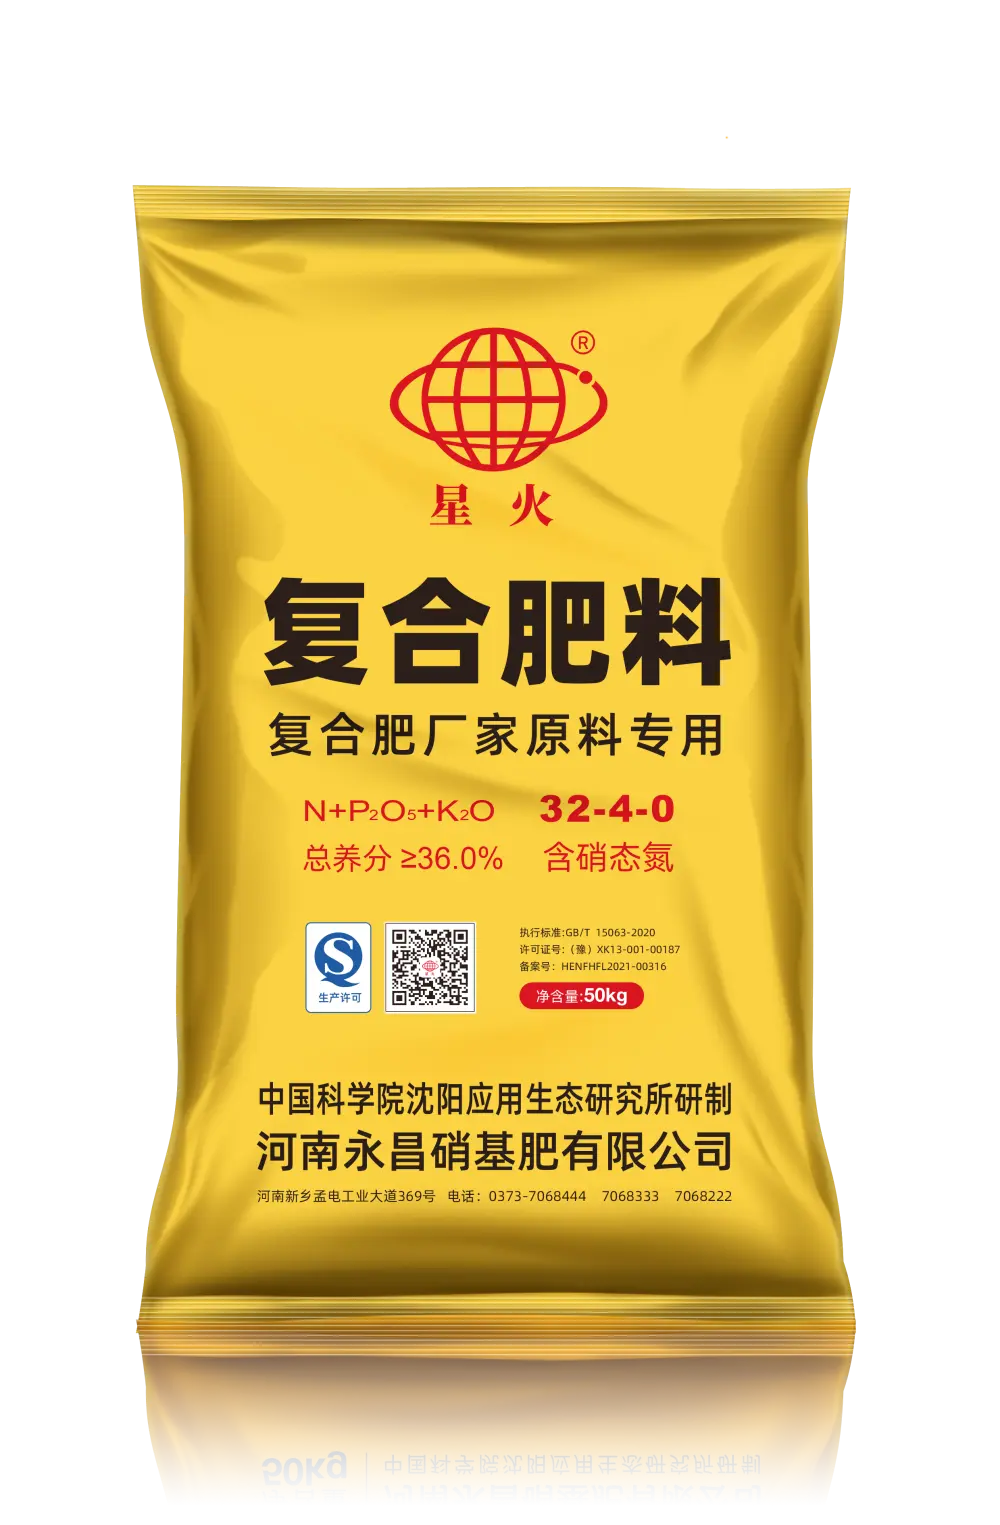
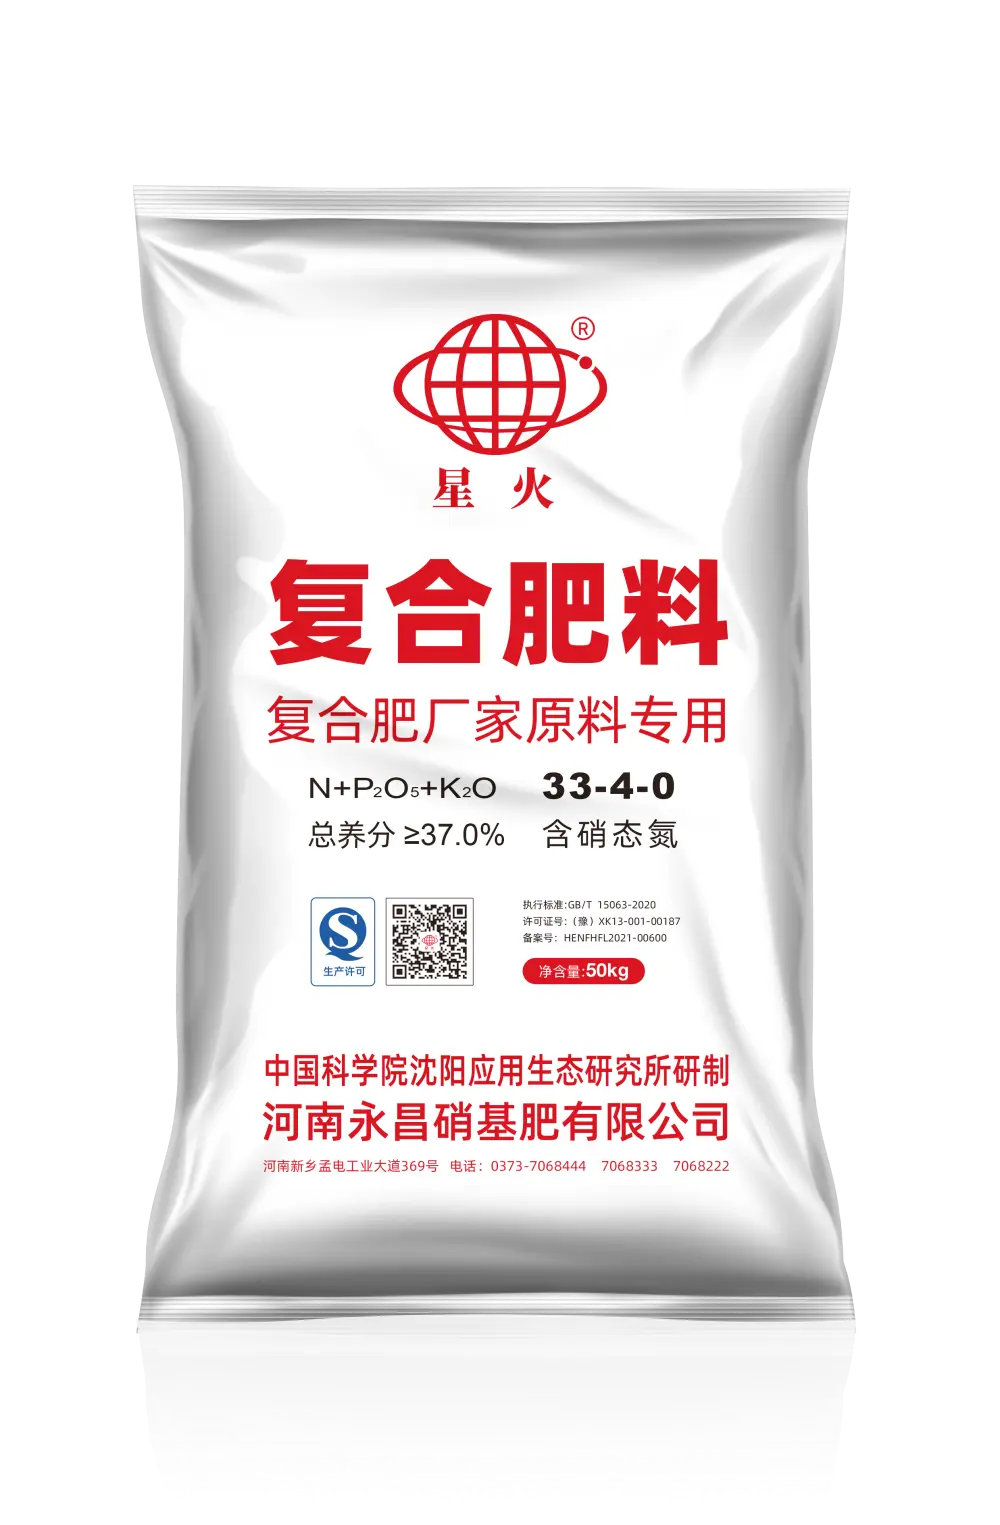
Browse our extended product portfolio engineered for industrial catalyst synthesis, mineral flotation, metallurgical treatment, and agricultural soil fortification.
 Nitro Fertilizer